The planned process
From graded scrap to cast anode, in five controlled stages.
A single duty furnace with a standby unit is designed to hold continuity; oxidation and reduction will set chemistry before molten copper is cast on the rotary disc.
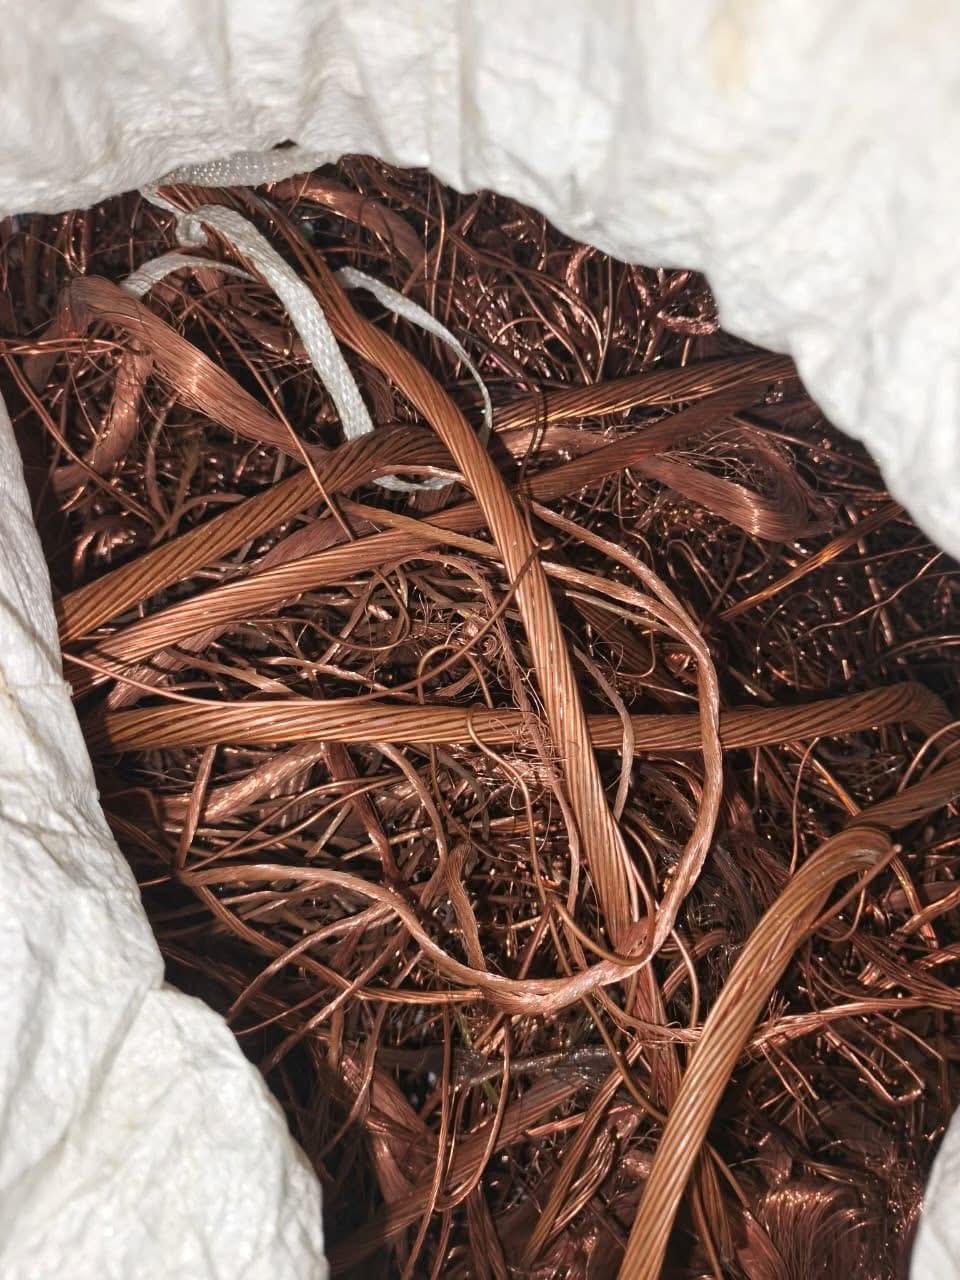
- 01 Intake & sortCopper scrap graded to No.1 bare-bright (~99%+ Cu) and No.2 light/armature (~94–97% Cu). Feed is scrap only — no concentrate.
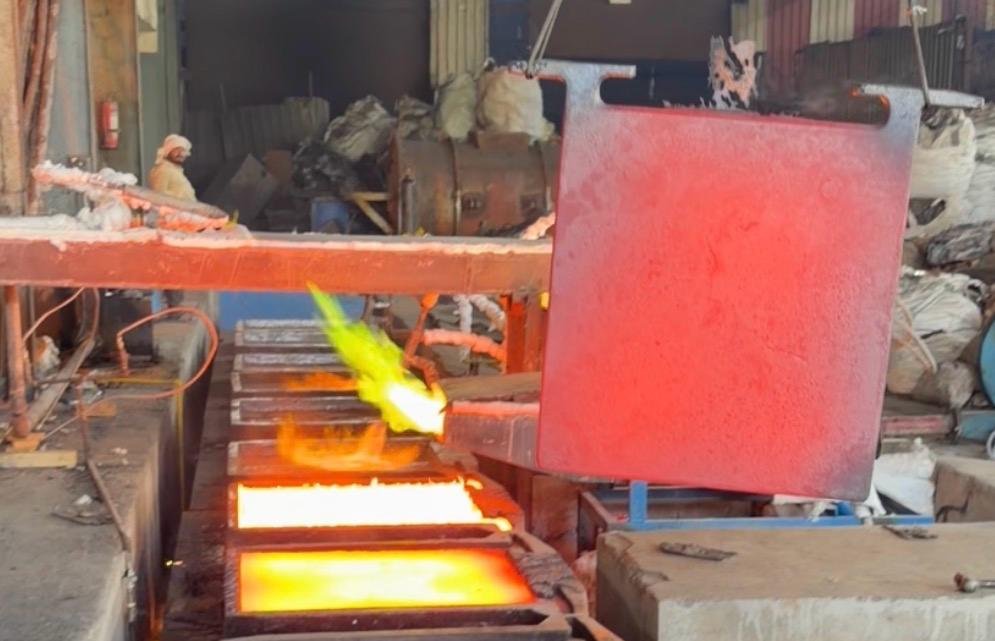
- 02 Melt & oxidationTilting rotary furnace fired with natural-gas oxy-fuel; oxidation slags off impurities from the melt.
- 03 Reduction & polingControlled reduction and poling bring the bath to ~99.3% Cu, refinery-grade for electrorefining.
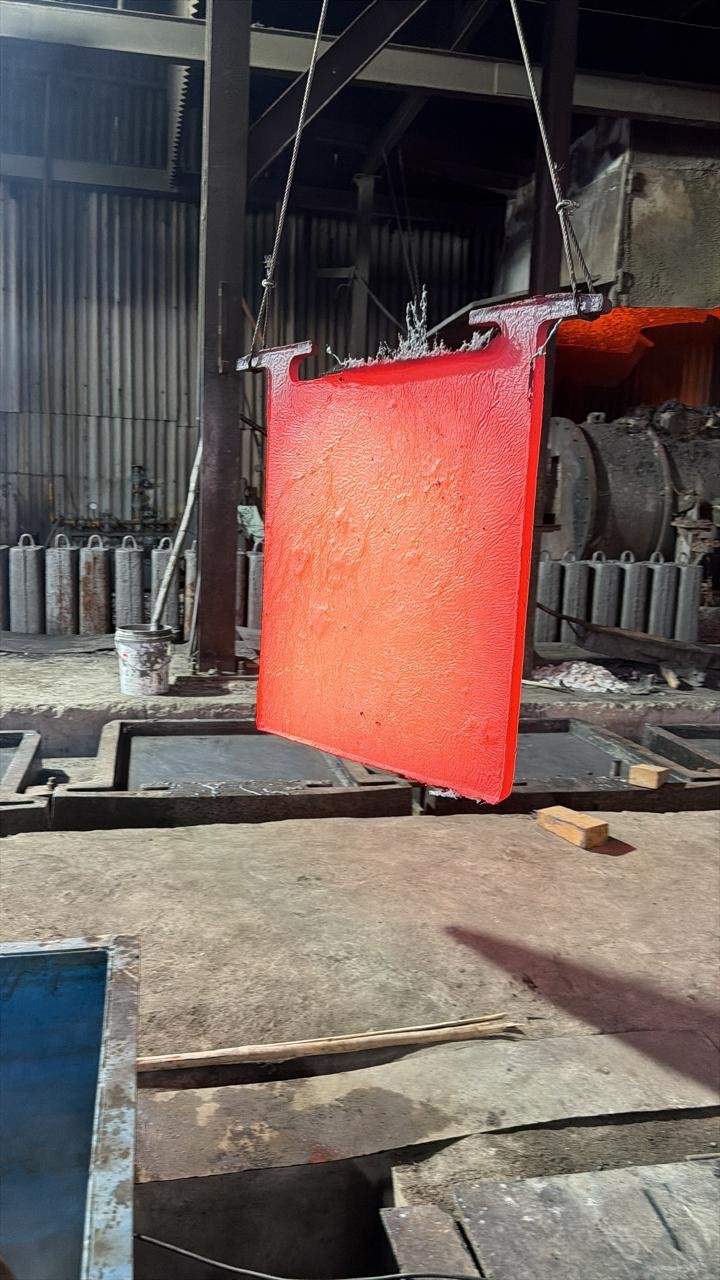
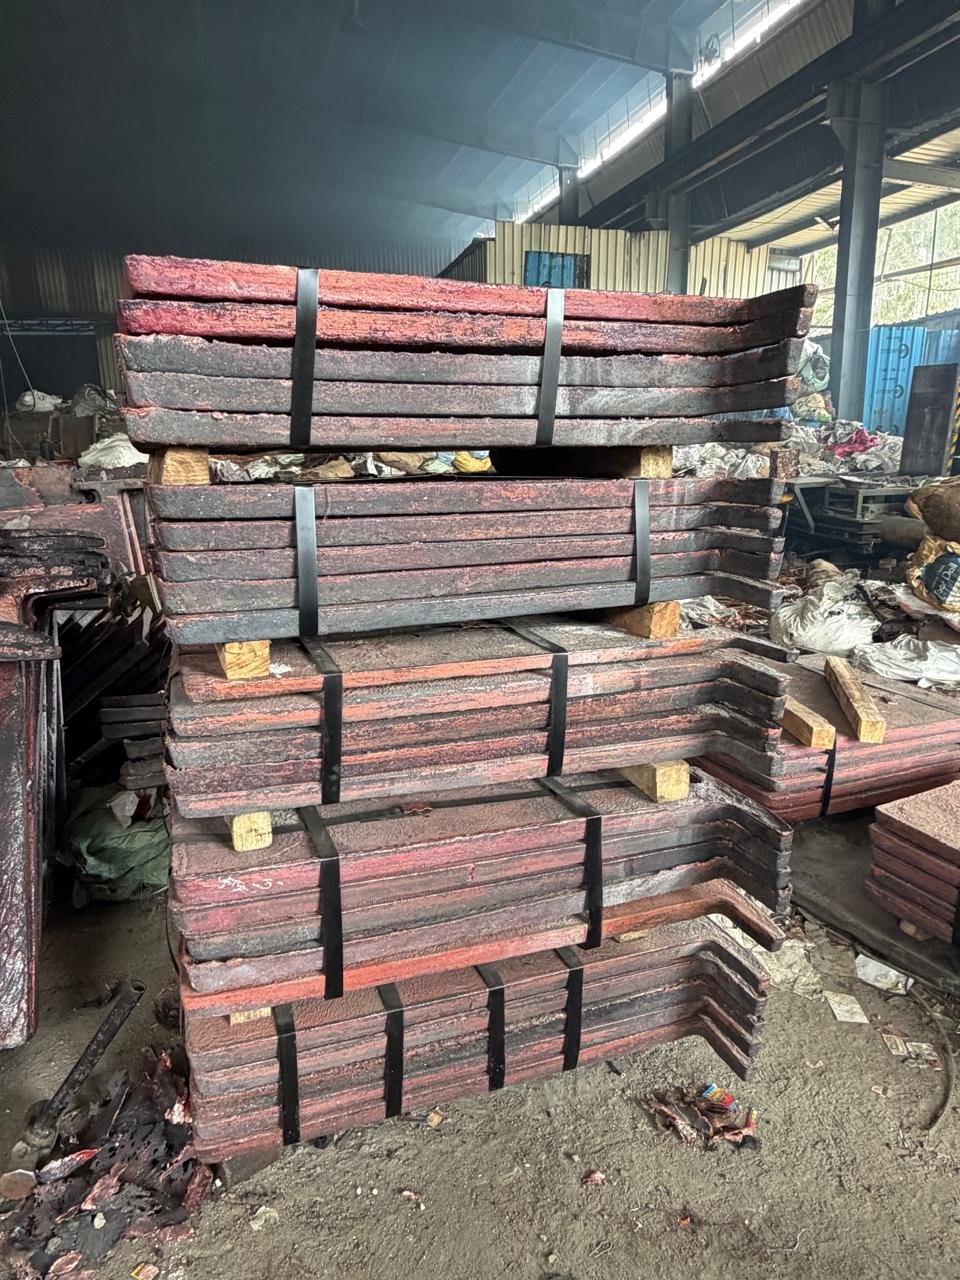
- 04 Disc castingMolten copper cast on a rotary disc machine into 330–380 kg anodes, ~960×960 mm with two cast lugs.
- 05 Cooling & QAAnodes cooled, weighed and checked to ≤±3 kg tolerance; ≥98% qualification across ~130–150 anodes/day.

{{ plateNum }} / 05
{{ plateTitle }}
Representative imagery
Next — The product
The first step toward refined copper.